Conveyor System for Material Handling: Types, Benefits and Industrial Applications
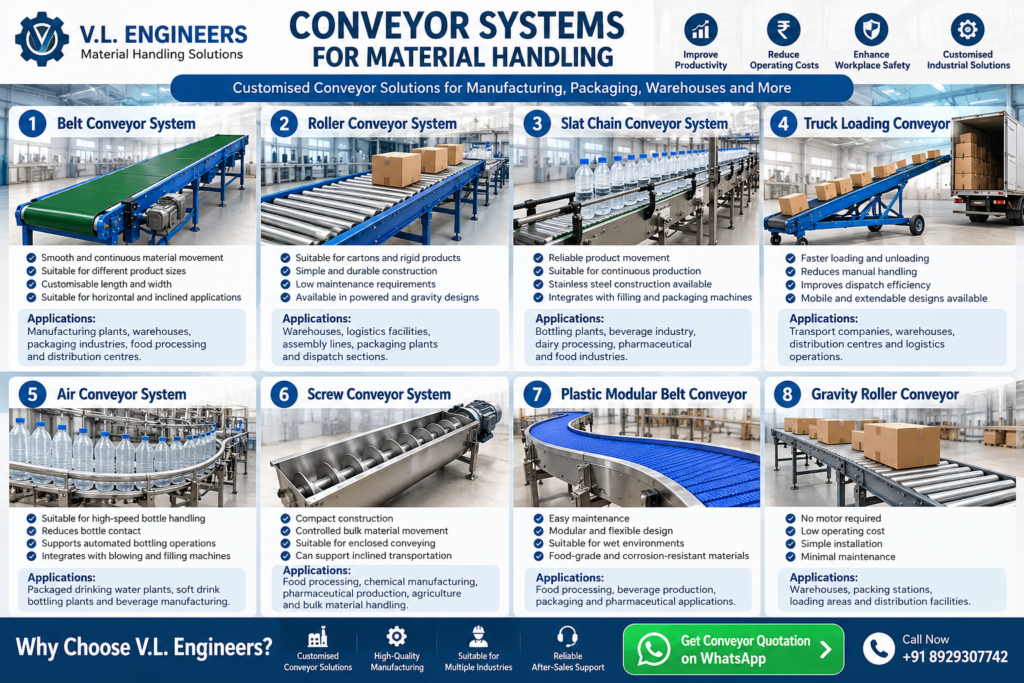
Efficient material handling is essential for maintaining productivity, reducing unnecessary manual work and ensuring smooth industrial operations.
In manufacturing plants, warehouses, packaging facilities and bottling industries, moving products safely and consistently between different processes can be challenging.
A conveyor system for material handling provides a practical solution by transporting materials, cartons, bottles, packages and industrial components through a controlled mechanical system.
Modern industrial conveyor systems help businesses improve material flow, reduce repetitive handling and support efficient production processes.
At V.L. Engineers, we manufacture customised conveyor systems for manufacturing, packaging, bottling, warehousing and industrial material handling applications.
Our conveyor solutions are designed according to product characteristics, required capacity, operating conditions and available installation space.
This guide explains the different types of conveyor systems, their working principles, industrial applications, benefits and important factors to consider before purchasing.
What Is a Conveyor System for Material Handling?
A conveyor system for material handling is mechanical equipment used to transport products or materials from one location to another within an industrial facility.
Depending on the application, conveyor systems may use moving belts, rotating rollers, chains, modular surfaces or other conveying mechanisms.
These systems are commonly installed between production machines, packaging stations, assembly lines, storage areas and dispatch sections.
What Materials Can Conveyor Systems Handle?
Industrial conveyor systems can transport a wide range of materials, including:
- Cartons and packaging boxes
- Plastic and glass bottles
- Bags and sacks
- Food and beverage products
- Pharmaceutical containers
- Industrial components
- Raw materials
- Finished goods
- Parcels and warehouse packages
How Does a Material Handling Conveyor System Work?
The operating principle of a conveyor system depends on its mechanical design.
Most powered conveyor systems use an electric motor connected to a drive mechanism that moves a belt, chain or series of rollers.
Step 1: Material Loading
Products are placed onto the conveyor manually or transferred from another machine.
Step 2: Conveyor Movement
The drive system moves the conveyor belt, rollers or chains at the required operating speed.
Step 3: Material Transportation
Products travel along a predetermined route towards the next processing or handling station.
Step 4: Product Transfer
Materials are transferred to packaging machines, production equipment, storage locations or dispatch areas.
Step 5: Continuous or Controlled Operation
Depending on the application, the conveyor operates continuously or intermittently.
Advanced conveyor installations may incorporate sensors, variable frequency drives, programmable logic controllers and automated product detection systems.
These features can support improved process control and integration with other industrial equipment.
Industries Using Conveyor Systems for Material Handling
Industrial conveyors are used across a wide range of manufacturing and logistics applications.
Food Processing Industry
Conveyor systems transport packaged food, containers and selected ingredients between processing and packaging stations.
Suitable materials and hygienic construction are important for food-related applications.
Beverage and Bottling Industry
Conveyors connect bottle blowing, rinsing, filling, capping, labelling and packaging machines.
Air conveyors, slat chain conveyors and modular belt conveyors are commonly used in different sections of bottling lines.
Pharmaceutical Industry
Conveyor systems support the controlled movement of bottles, containers and packaged pharmaceutical products.
Equipment selection should reflect applicable hygiene, cleaning and quality requirements.
Warehouse and Logistics Industry
Warehouse conveyor systems move cartons, parcels and packaged products between sorting, packing, storage and dispatch areas.
Manufacturing Industry
Industrial conveyors transport components, raw materials and finished goods between production processes.
Packaging Industry
Packaging conveyors connect filling, inspection, sealing, labelling, carton packing and dispatch operations.
Chemical In dustry
Specially designed conveyor systems can handle compatible packaged chemicals and selected bulk materials.
Material compatibility and relevant safety requirements must be considered during system design.
How to Choose the Right Conveyor System for Your Industry
Selecting the correct conveyor system is important for operational reliability and long-term performance.
Before purchasing, consider the following factors.
Material Type
Identify whether the conveyor will transport bottles, cartons, bags, powders, containers or industrial components.
Product Weight and Dimensions
Determine the maximum product weight, dimensions and load distribution.
These factors influence conveyor width, structural design and drive selection.
Required Conveyor Speed
Choose a suitable operating speed based on production capacity and the performance of connected equipment.
Conveyor Length and Layout
Measure the available installation space and required transportation distance.
Consider straight, inclined, curved and multi-level conveying arrangements where appropriate.
Construction Material
Select suitable construction materials according to operating conditions.
Common options include mild steel, stainless steel and aluminium profiles.
Automation Requirements
Determine whether the application requires manual operation, motorised conveying or integration with automated production equipment.
Maintenance and Safety
Consider cleaning accessibility, spare parts, guarding, emergency stops and maintenance requirements.
A conveyor manufacturer should evaluate these factors before recommending a suitable configuration
Belt Conveyor vs Roller Conveyor: Which Is Better?
Belt conveyors and roller conveyors are two widely used material handling solutions.
However, they are designed for different product characteristics.
Choose a Roller Conveyor When:
-
Products have rigid, stable bottom surfaces.
-
Cartons need transportation between packaging stations.
-
Gravity-based movement is suitable.
-
The application requires straightforward carton handling.
Neither system is universally better.
The correct choice depends on product dimensions, weight, stability, required throughput and conveyor layout.
Conveyor System Maintenance Tips
Regular maintenance is essential for maintaining reliable conveyor operation.
Important maintenance activities include:- Inspecting belts, rollers and chains
- Checking belt alignment and tension
- Lubricating components according to manufacturer recommendations
- Inspecting motors and gearboxes
- Cleaning accumulated dust and debris
- Checking emergency stops and safety guards
- Replacing worn or damaged components
- Following appropriate isolation and lockout procedures before maintenance
Why Choose V.L. Engineers for Conveyor Systems?
Choosing the right conveyor manufacturer is important for achieving reliable material movement and efficient industrial operations.
V.L. Engineers manufactures industrial conveyor systems for manufacturing, bottling, packaging, warehousing and material handling applications.
We understand that different industries require different conveyor configurations.
Our customised conveyor solutions are designed according to product characteristics, required production capacity, installation space and operating conditions.
Our Conveyor Product Range
V.L. Engineers offers:
-
Belt Conveyor Systems
-
Roller Conveyor Systems
-
Slat Chain Conveyor Systems
-
Truck Loading and Unloading Conveyors
-
Air Conveyor Systems
-
Screw Conveyor Systems
-
Plastic Modular Belt Conveyors
-
Gravity Roller Conveyors
-
Customised Material Handling Conveyor Systems
Customised Conveyor Solutions
Our conveyor systems can be configured according to:
Product type and dimensions
Required conveyor capacity
Conveyor length and width
Factory layout
Operating environment
Construction material
Automation requirements
Integration with existing equipment
Our objective is to provide practical industrial conveyor solutions that support smooth material movement, reliable operation and efficient production workflows.
Frequently Asked Questions About Conveyor Systems
FAQ 1: What is a conveyor system for material handling?
A conveyor system is mechanical equipment used to transport products, packages or materials between different locations within factories, warehouses and industrial facilities.
FAQ 2: Which conveyor system is best for industrial material handling?
The best conveyor depends on the product and application. Belt conveyors are suitable for many packaged products, while roller conveyors are commonly used for cartons and rigid-bottom goods.
FAQ 3: What are the advantages of industrial conveyor systems?
Industrial conveyor systems improve material flow, reduce repetitive manual handling, support production efficiency and help organise transportation within industrial facilities.
FAQ 4: Where are conveyor systems commonly used?
Conveyor systems are widely used in manufacturing plants, warehouses, bottling facilities, food processing units, pharmaceutical industries and packaging operations.
FAQ 5: Can conveyor systems be customised?
Yes. Conveyor systems can be customised according to product dimensions, weight, required speed, factory layout, construction material and automation requirements.
FAQ 6: What is the difference between powered and gravity conveyors?
Powered conveyors use a motor-driven mechanism to transport products. Gravity conveyors rely on gravity or manual force.
FAQ 7: How much does a conveyor system cost in India?
Conveyor system prices in India depend on the conveyor type, dimensions, load capacity, construction material, drive system, automation features and application requirements.
For accurate pricing, businesses should request a quotation based on their technical requirements.
FAQ 8: How do I choose a conveyor system manufacturer in India?
Consider the manufacturer’s product range, technical capabilities, customisation options, construction quality, service support and experience with similar industrial applications.
FAQ 9: Can conveyor systems integrate with existing production lines?
Yes. Suitable conveyor systems can be designed to integrate with existing production, packaging, filling and dispatch equipment.
Compatibility depends on the mechanical layout, operating speeds and control requirements.
FAQ 10: What information is required for a conveyor quotation?
A manufacturer will typically need the product type, dimensions, weight, required capacity, conveyor length, installation layout and operating conditions.
Providing these details helps the manufacturer recommend a suitable system.
Conclusion
A conveyor system for material handling is an important solution for businesses seeking organised, consistent and efficient material transportation.
From belt conveyors and roller conveyors to air conveyors, screw conveyors and truck loading systems, different conveyor technologies serve different industrial requirements. Choosing the correct conveyor can help improve production workflow, reduce repetitive handling and support long-term operational efficiency. Businesses should select conveyor equipment based on actual product characteristics, operating conditions and production requirements.
Looking for a Reliable Conveyor System Manufacturer in India?
V.L. Engineers manufactures customised industrial conveyor systems for manufacturing plants, bottling lines, warehouses, packaging facilities and other material handling applications.
Whether you require a belt conveyor, roller conveyor, slat chain conveyor, air conveyor or truck loading system, our team can discuss suitable configurations for your application.